Leave Your Message

China Top Thermohydraulic Coating Automatic Cutting Machine

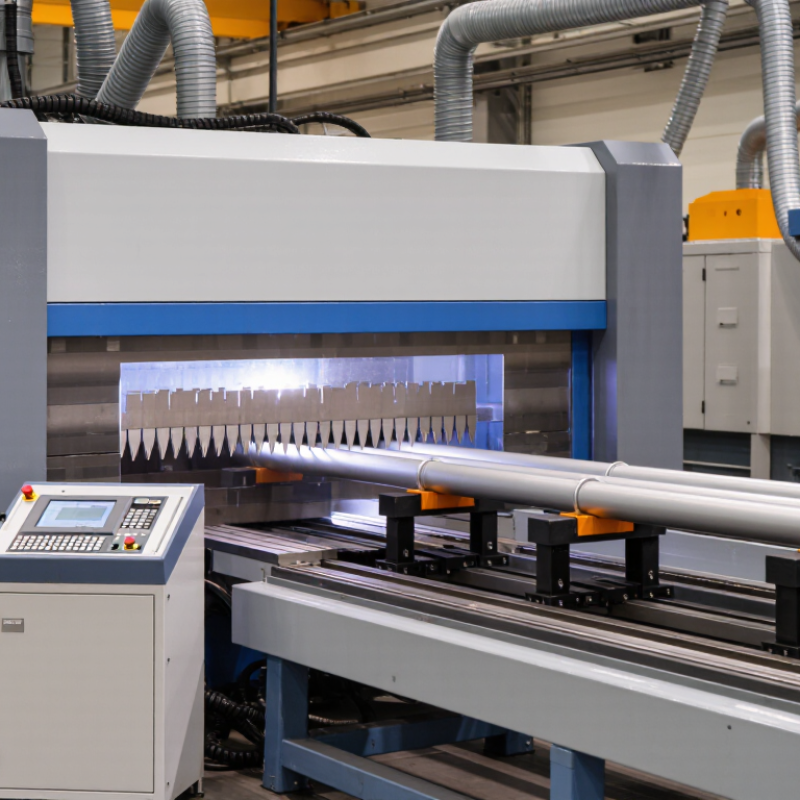
China Top Thermohydraulic Coating Automatic Cutting Machine technology supports accurate preparation of coated tubes, panels, and industrial components. It is designed for production environments requiring repeatable cutting, clean edges, and controlled material handling. The keyword Thermohydraulic Coating Automatic Cutting reflects a specialized process, not merely a general cutting solution.

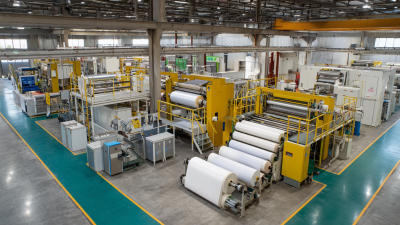
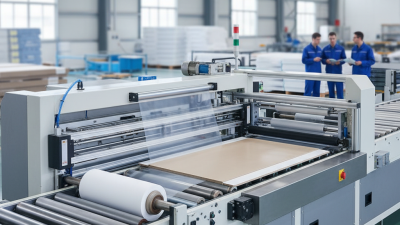
In practical use, operators load coated workpieces onto a guided table. Sensors check positioning before the cutting cycle begins. A programmable controller then manages feed speed, cutting length, and return movement. This reduces manual measurement errors during repeated production tasks. The machine may also connect with dust extraction and collection systems. That detail matters when coating residues accumulate around the cutting area.

Manufacturers in China commonly provide equipment customization for different dimensions, coating thicknesses, and factory layouts. Reliable suppliers should explain blade selection, machine capacity, maintenance intervals, and safety protections clearly. Technical drawings, test records, and traceable component information can support professional purchasing decisions. However, performance depends on material hardness, operator training, and correct calibration. No machine is flawless. This deserves more scrutiny.

A credible evaluation should include sample cutting tests with the customer’s actual coated materials. Inspectors can measure edge quality, dimensional variation, noise, and production speed. They should also review emergency stops, guarding, electrical documentation, and spare-part availability. These checks connect promotional claims with observable evidence. For buyers comparing China Top Thermohydraulic Coating Automatic Cutting Machine suppliers, transparent communication remains essential. The strongest choice is not always the fastest machine. It is the system that delivers stable results, practical support, and safe operation over time.
China Top Thermohydraulic Coating Automatic Cutting Machine

Thermohydraulic Coating Cutting Machines: Definition and Applications

Thermohydraulic coating cutting machines process coated sheets, films, and composite materials. These coatings help surfaces resist heat, hydraulic oil, pressure, abrasion, and corrosion. The machine does not apply the coating. It cuts prepared materials into accurate shapes for later assembly.

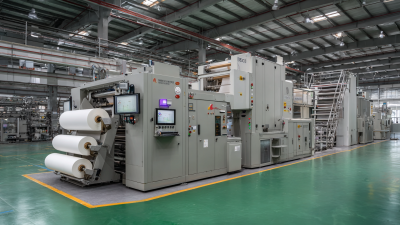
Automatic cutting systems use digital drawings, controlled feed rollers, and adjustable cutting tools. Operators may select an oscillating knife, rotary blade, or another suitable method. The choice depends on coating thickness and flexibility. Common applications include hydraulic seals, heat-resistant liners, insulation panels, protective gaskets, and machine covers. They support equipment used in fluid control, industrial heating, transport, and energy facilities.

Practical setup matters. Blade pressure, cutting speed, and material tension can change edge quality. A test cut should come before full production. Operators should inspect dimensions, delamination, burrs, and surface damage. A clean edge is not guaranteed. Some hard coatings crack when the tool moves too quickly. Thermal cutting can also create fumes, so ventilation and material safety data deserve attention. Automatic systems improve repeatability, but they do not replace skilled inspection. In real workshops, small material variations still cause unexpected results. Recording settings and rejected parts helps engineers refine future batches.

China Top Thermohydraulic Coating Automatic Cutting Machine - Thermohydraulic Coating Cutting Machines: Definition and Applications

Data Dimension Typical Specification or Value Technical Significance Typical Application
Machine definition An automated cutting system used to section coated sheets, films, laminates, tubes, panels, or test coupons with thermally and hydraulically protective coating layers. Combines controlled feeding, positioning, cutting, and part handling while helping preserve coating integrity. Coated metal processing, pipe protection, thermal barrier materials, and laboratory sample preparation.
Common coating types Thermal-spray coatings, polymer coatings, epoxy systems, elastomeric layers, ceramic-filled coatings, and multilayer protective films. Different hardness, thickness, elasticity, and heat sensitivity require different cutting tools and process settings. Wear protection, corrosion protection, thermal insulation, and fluid-handling components.
Suitable workpiece materials Coated steel, stainless steel, aluminum, composite panels, polymer sheets, rubber-lined parts, and flexible coating films. Material compatibility affects cutting force, edge quality, heat generation, and tool wear. Industrial equipment, storage tanks, pipelines, ducts, and fabricated coated components.
Cutting methods CNC knife cutting, rotary blade cutting, abrasive cutting, sawing, waterjet cutting, or laser cutting, depending on the substrate and coating. The selected method controls burr formation, delamination, thermal damage, and dimensional accuracy. Sheet cutting, pipe sectioning, gasket production, panel profiling, and coating test specimens.
Typical coating thickness Approximately 25 micrometers to several millimeters, depending on the coating system and intended service. Thickness influences blade selection, cutting speed, clamping force, and the risk of coating separation. Thin protective films, heavy-duty polymer linings, thermal barrier layers, and wear-resistant surfaces.
Dimensional control Typical automated positioning repeatability: about ±0.05 mm to ±0.20 mm, depending on machine design, tool, and material. Consistent positioning improves part interchangeability and reduces manual trimming. Precision panels, repeat production, inspection samples, and coated component fabrication.
Automatic feeding Roll feeding, sheet loading, conveyor transfer, or programmable indexing with sensors for material presence and alignment. Reduces manual handling and supports stable production cycles. Continuous film processing, sheet cutting, and medium- to high-volume production.
Control system Programmable motion control with digital recipe storage, speed adjustment, length setting, sensor feedback, and emergency-stop functions. Allows repeatable process parameters for different coating materials and product sizes. Multi-format production, job changeovers, quality-controlled manufacturing, and sample preparation.
Cutting speed Common automated systems provide adjustable speeds from low-speed precision cutting to several hundred millimeters per second, depending on the tool and material. Adjustability helps balance productivity against heat buildup, deformation, and edge quality. Flexible coating films, rigid panels, composite materials, and coated metal sections.
Workholding Vacuum tables, clamps, rollers, fixtures, or contour supports selected according to workpiece geometry. Stable workholding limits vibration, movement, coating lift, and dimensional variation. Flat sheets, curved pipe sections, irregular panels, and flexible coated materials.
Edge-quality requirements Clean separation with controlled burrs, limited delamination, minimal chipping, and no unacceptable heat-affected damage. Edge quality is important when the cut surface will be sealed, bonded, inspected, or exposed to corrosive service. Pipe ends, gasket surfaces, laboratory coupons, and coated assemblies requiring further joining.
Dust and fume control Local extraction, enclosed cutting zones, filtration, and suitable personal protective equipment may be required. Controls airborne particles and fumes generated by abrasive, laser, or mechanically cut coating materials. Industrial workshops, enclosed production lines, and coating inspection laboratories.
Quality inspection Visual inspection, dimensional measurement, coating-thickness checks, adhesion assessment, and surface-defect inspection. Verifies that cutting has not damaged the coating system or altered the test area. Process qualification, incoming inspection, failure analysis, and production quality control.
Main benefits Repeatable cuts, reduced labor, programmable formats, improved material utilization, and more consistent handling. Automation improves process stability when the cutting parameters are matched to the coating and substrate. Batch production, standardized test pieces, custom shapes, and coating component preparation.

Note: Actual performance depends on the coating chemistry, substrate, thickness, geometry, cutting tool, workholding method, and process settings. The ranges shown are typical industry-oriented values rather than universal machine specifications.
Machine Architecture: CNC Control, Blades, and ±0.1 mm Cutting Accuracy

China Top Thermohydraulic Coating Automatic Cutting Machine

A modern thermohydraulic coating cutter depends on architecture, not marketing language. Its CNC controller coordinates feed speed, blade position, clamping pressure, and tool compensation. Closed-loop feedback matters when coating thickness changes across a panel. The International Federation of Robotics reported 4.28 million industrial robots operating worldwide in 2023. This figure appears in its World Robotics 2024 report. It reflects the wider shift toward programmable production.

The ±0.1 mm specification needs careful interpretation. ISO 230-2:2014 separates positioning accuracy from repeatability, reversal error, and measurement uncertainty. A machine may reach ±0.1 mm during controlled tests. Performance can change after thermal growth, vibration, or blade wear. A practical acceptance test should use calibrated gauges, repeated samples, and several cutting directions. I would record results at startup and after continuous operation.

Blade architecture is equally important. A rigid spindle and short tool overhang reduce cutting vibration. Stable vacuum or mechanical fixtures help prevent coating movement. The CNC system should apply kerf compensation as blade diameter changes. Operators also need alarms for drift, overload, and encoder faults. Real production is less tidy. Dust, uneven coating, and hurried setup can reduce accuracy. The target becomes credible only when controls, blades, fixtures, and inspection records work together.

Operating Workflow: Loading, Positioning, Cutting, and Material Collection

China Top Thermohydraulic Coating Automatic Cutting Machine

The operating workflow begins with controlled loading. Operators place coated tubes or sheets onto the feed table, keeping edges clear of clamps. A visual inspection checks coating thickness, surface damage, and material direction. This matters because uneven coating can shift during cutting. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. That growth reflects a wider move toward repeatable, monitored production.

Positioning follows loading. Sensors identify length, diameter, and reference marks before pneumatic or servo clamps secure the material. The cutting head then follows programmed speed and pressure settings. A slower approach can reduce coating chipping, while excessive pressure may deform the substrate. In practice, this setting is easy to underestimate. After cutting, the collection conveyor separates finished pieces from offcuts. Operators should check cut edges, count parts, and record abnormal vibration or dust.

Tips: Keep the loading surface clean. Confirm sensor calibration each shift. Use a test cut after material changes. Do not rely only on the control screen; inspect the first finished piece by hand. ISO 12100 risk-assessment principles support guarding, safe access, and controlled maintenance. Still, real workshops reveal gaps. Small alignment errors can become large batch defects. Reviewing rejected pieces weekly helps improve settings and operator training.

Key Parameters: 20–60 m/min Speed and Coating Thickness Control

China Top Thermohydraulic Coating Automatic Cutting Machine

A thermohydraulic coating automatic cutting machine must balance speed with coating stability. Its operating range of 20–60 m/min supports different production conditions. Lower speeds help when materials require careful handling. Higher speeds improve output when the coating has already stabilized.

Thickness control deserves closer attention. A calibrated sensor can monitor the coating layer during continuous operation. The control system then adjusts application pressure, temperature, or material flow. Stable tension also matters, because uneven tension can create thin edges or local buildup. Small changes become visible under strong inspection lighting.

Real production is less perfect. Dust, roller wear, and temperature shifts can affect readings. Operators should check samples at regular intervals, not trust the display alone. A micrometer or suitable thickness gauge provides useful verification. Cutting accuracy also depends on web alignment and blade condition. Dull blades may pull the coated material instead of cutting cleanly.

Keep records.

The 20–60 m/min range should be tested against the actual substrate, coating formulation, and required thickness. A practical trial may reveal that maximum speed reduces consistency. That finding is not a failure; it shows where process control needs refinement. Reliable operation comes from measured adjustments, documented maintenance, and trained handling rather than speed alone.

China Top Thermohydraulic Coating Automatic Cutting Machine

Reference operating parameters: line speed from 20–60 m/min with adjustable coating thickness control.

The chart presents practical reference setpoints across the machine’s stated speed range. Coating thickness values are shown in micrometres and should be verified against material type, coating formulation, web tension, and production conditions.

Safety and Standards: IEC 60204-1, Guarding, and Emergency Systems

China Top Thermohydraulic Coating Automatic Cutting Machine

A thermohydraulic coating automatic cutting machine needs more than accurate blades and stable pressure. Its electrical equipment should be designed and assessed against IEC 60204-1 requirements. This standard addresses control circuits, protective bonding, isolation, wiring, and emergency stop functions. During commissioning, technicians should verify voltage, grounding continuity, enclosure condition, and control-panel labeling.

Guarding must keep operators away from cutting zones, heated surfaces, moving clamps, and stored hydraulic energy.

Fixed guards should resist removal without tools. Interlocked access doors can stop hazardous motion when opened. The safety distance must match the machine’s movement and the operator’s reach. Small gaps are easy to miss.

Emergency systems require practical testing.

A reachable emergency-stop device should halt dangerous motion without creating a new hazard. Resetting it must not restart the machine automatically. Operators need clear instructions near loading and unloading areas. Test results should record the date, device location, stopping behavior, and corrective action. Real workshops are dusty, noisy, and rushed; safety checks must reflect those conditions. One weakness remains common: teams may test the button but overlook delayed hydraulic movement. That detail deserves another review.